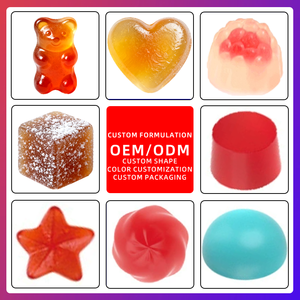
Select from our market-validated portfolio of turnkey formulations or request bespoke contract manufacturing engineered for rapid market deployment.
In the rapidly expanding global nutraceutical sector, selecting top trusted softgel capsules manufacturers is the single most critical supply chain decision for wellness brand owners, pharmaceutical procurement directors, and contract distributors. Softgel encapsulation technology represents the gold standard for delivering hydrophobic nutrients, lipophilic bioactive oils, and oxygen-sensitive active ingredients. Unlike traditional hard capsules or compressed tablets, softgels provide a hermetically sealed, tamper-evident delivery system that maximizes gastrointestinal absorption and safeguards active compounds against oxidative degradation.
Softgel encapsulation utilizes self-emulsifying drug delivery systems (SEDDS) and lipid carriers to dissolve insoluble active compounds (e.g., CoQ10, Astaxanthin, Vitamin D3/K2, Phytosterols). This lipid matrix enhances intestinal permeability, yielding up to 400% higher clinical absorption compared to dry powder dosage formats.
Sensory degradation and rancidity are major risks for Omega-3 EPA/DHA fish oils, Evening Primrose oil, and botanical lipids. Hermetic rotary die encapsulation eliminates headspace oxygen, ensuring peroxide values (PV) remain well within strictly regulated USP and GOED safety thresholds throughout shelf-life.
State-of-the-art positive displacement micro-metering pumps inject liquid fill matrices into gel ribbons with mass variance under ±1.5%. This guarantees consistent API potency per unit, eliminating potency drift commonly observed in blended powder capsules.
Compare core encapsulation shell polymer parameters to select the optimal technology for your target demographics and climate conditions.
| Encapsulation Shell Parameter | Bovine / Porcine Gelatin | Plant-Based Tapioca Starch | Enteric Coated Gelatin |
|---|---|---|---|
| Primary Composition | Pharmaceutical Grade Gelatin (150-200 Bloom) | Modified Tapioca Starch + Iota-Carrageenan | Phthalate-Free Methacrylic Polymer Coating |
| Thermal Stability Limit | Up to 32°C (Risk of shell melting above 38°C) | High Thermal Resistance (Up to 48°C) | Up to 35°C (Coating integrity preserved) |
| Cross-Linking Susceptibility | Moderate to High (Requires Succinylation) | Zero Susceptibility (Non-Protein Matrix) | Low (Protected by outer polymer layer) |
| Disintegration Time | 5 – 15 Minutes (Gastric Fluid) | 10 – 20 Minutes (Gastric Fluid) | > 120 Mins (Gastric), < 30 Mins (Intestinal) |
| Target Fill Applications | Standard Oils, Fat-Soluble Vitamins | Vegan Omega-3 (Algal DHA), High Heat Regions | Probiotics, Acid-Sensitive Enzymes, Garlic/Fish Oils |
| Dietary Compliance | Kosher/Halal (Cert. Required) | 100% Vegan, Vegetarian, Non-GMO | Depends on Base Shell Material |
As consumer purchasing behavior pivots toward clean-label transparency, ethical sourcing, and specialized clinical outcomes, supplement brand managers must align with contract manufacturers capable of navigating next-generation manufacturing paradigms.
While animal gelatin historically dominated contract manufacturing, global procurement data indicates a 22.4% year-over-year surge in demand for vegetarian softgel capsules. Derived from modified cassava tapioca starch, plant softgels offer unmatched physical stability in high-humidity (Zone IVb) shipping corridors across Southeast Asia, the Middle East, and Latin America, while fully satisfying Halal, Kosher, and Vegan consumer requirements.
Advanced buyers are transitioning away from post-encapsulation spray coatings in favor of intrinsically acid-resistant polymer matrix shells. This innovation protects delicate active fills—such as live probiotic strains, SAM-e, and proteolytic enzymes—from stomach gastric acid destruction, delivering the active payload directly to the small intestine without unpleasant reflux or regurgitation.
Modern high-volume manufacturing facilities integrate Near-Infrared (NIR) spectroscopic sensors directly into gelatin ribbon spreading lines and fill injection manifolds. Real-time PAT monitoring continuously evaluates ribbon thickness, moisture levels, seam integrity, and fill mass, reducing batch failure rates to less than 0.005%.
Following the European Food Safety Authority (EFSA) ban on Titanium Dioxide (E171) due to genotoxicity concerns, tier-one manufacturers have engineered high-opacity natural shell colorants. Utilizing natural calcium carbonate, riboflavin, chlorophyllins, and apple extract concentrates, brands maintain vibrant, opaque capsule aesthetics while staying fully compliant with global food safety standards.
ProTech Health Sciences stands at the forefront of pharmaceutical and nutraceutical contract manufacturing. Operating state-of-the-art cGMP certified facilities equipped with high-speed automated rotary die encapsulation machinery, we deliver end-to-end turnkey solutions for brand owners in over 40 global markets.
Our cleanrooms operate under Class 100,000 (ISO Level 8) environmental standards. We maintain active compliance certifications including US FDA Registration, ISO 22000, ISO 9001:2015, HACCP, and international Halal standard compliance.
Streamline your time-to-market with our extensive portfolio of pre-formulated, stability-tested master formulas—spanning sports nutrition, anti-aging, beauty-from-within, cardiovascular health, and pet supplement solutions.
Every batch undergoes rigorous quality testing utilizing High-Performance Liquid Chromatography (HPLC), Gas Chromatography-Mass Spectrometry (GC-MS), and ICP-MS for heavy metal and micro-contamination screening.
Detailed technical and commercial insights to simplify your contract manufacturing evaluation and vendor auditing processes.