Explore our benchmark private label effervescent formulations manufactured under pharmaceutical-grade HVAC environmental controls (RH < 20%).
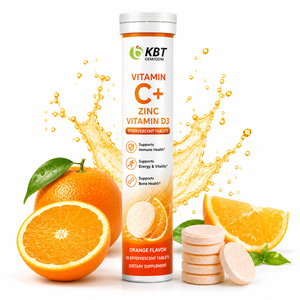
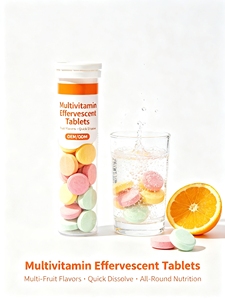
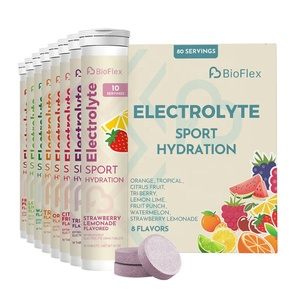
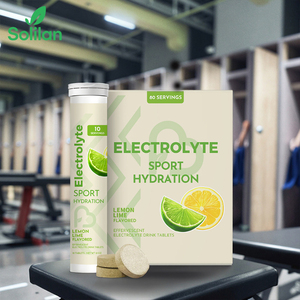
In the evolving landscape of global nutraceuticals and dietary supplements, effervescent dosage forms represent one of the fastest-growing market segments. Brand owners, pharmaceutical distributors, and retail chain buyers are increasingly pivoting away from traditional swallowed tablets and hard-gel capsules toward effervescent tablets. This transition is propelled by two major forces: unmatched patient compliance and accelerated active ingredient bioavailability.
Unlike conventional solid dosage forms that require mechanical breakdown inside the human gastrointestinal tract, effervescent tablets undergo an engineered acid-base carbonation reaction upon contact with water. The immediate release of carbon dioxide (CO2) creates a buffered aqueous solution that accelerates gastric emptying, minimizes localized stomach irritation, and significantly expands the surface area for nutrient absorption in the small intestine.
Engineering stable, non-degrading, and fast-dissolving effervescent tablets requires rigorous chemical balancing and specialized cleanroom environments. At ProTech Health Sciences, our R&D team balances stoichiometric proportions of organic acid donors with bicarbonate bases to achieve complete dissolution without leftover residue or cloudiness.
The core reaction relies on the interaction between an organic acid (typically anhydrous Citric Acid, Malic Acid, or Tartaric Acid) and an alkali carbonate source (Sodium Bicarbonate, Potassium Bicarbonate, or Sodium Carbonate):
C6H8O7 (Citric Acid) + 3 NaHCO3 (Sodium Bicarbonate) → Na3C6H5O7 (Sodium Citrate) + 3 H2O + 3 CO2 (Gas)
Maintaining exact stoichiometric ratios prevents taste bitterness, excessive sodium content, or incomplete effervescence. For low-sodium formulations, our chemists replace sodium bicarbonate with potassium or magnesium bicarbonate, delivering functional minerals alongside active nutrients.
Effervescent powders are intensely hygroscopic. Exposure to ambient humidity triggers premature reaction during blending or compression, leading to tablet swelling, capped tops, and reduced shelf-life. Top-tier effervescent factories implement specialized HVAC air handlers that enforce continuous environmental parameters:
| Technical Parameter | Standard Pill / Capsule OEM | ProTech Advanced Effervescent OEM | Procurement Impact & Benefit |
|---|---|---|---|
| Environmental RH Control | 45% – 60% Ambient RH | Strict < 20% RH HVAC Cleanroom | Prevents active oxidation & guarantees 24-month stability. |
| In-Vitro Dissolution Speed | 20 – 45 Minutes (Disintegration) | 60 – 120 Seconds (Complete Solution) | Rapid absorption, immediate hydration, zero pill swallow fatigue. |
| Gastric Mucosal Safety | High localized concentration risk | Fully buffered aqueous micro-dispersion | Gentle on sensitive stomach linings; no nausea after intake. |
| Packaging Integrity | Standard HDPE Bottles / Blisters | Desiccant-Cap Aluminum Tubes / Alu-Alu | Hermetic moisture protection suitable for tropical import zones. |
| Flavor Masking Tech | Basic outer coating | Micro-encapsulated active taste masking | Delivers crisp, refreshing taste even with bitter minerals/botanicals. |
As international buyers evaluate effervescent tablet contract manufacturers, several crucial product trends are shaping purchasing strategies across North America, Europe, Southeast Asia, and the Middle East:
Global consumers actively reject high-sugar energy or vitamin drinks. Leading brand buyers require natural sweetening systems utilizing Steviol Glycosides (Stevia), Erythritol, or Monk Fruit extracts. Formulations must maintain crisp taste profiles without artificial colorants, azorubine dyes, or chemical binders.
Single-ingredient Vitamin C tablets are being replaced by multi-target functional complexes. Current high-demand OEM formulations combine high-potency Vitamin C (1000mg) with Zinc Picolinate, Vitamin D3, Sambucus Nigra (Elderberry Extract), and essential hydration ions (Sodium, Potassium, Magnesium). This multi-active synthesis provides superior consumer value per tube.
The sports nutrition sector is adopting effervescent hydration tablets as eco-friendly replacements for single-use plastic electrolyte bottles. Lightweight, easily transportable tubes allow athletes to generate fresh electrolyte beverages on demand. The inclusion of natural caffeine from Guarana or Green Tea Extract provides clean energy without sugar crashes.
With over two decades of dedicated R&D and production mastery, ProTech Health Sciences empowers brands to launch compliant, market-leading effervescent formulations.
Fully certified under GMP, ISO 22000, ISO 9001:2015, HACCP, and Halal standards. Comprehensive COA documentation provided for every batch.
Accelerate your brand launch with our extensive library of pre-tested, high-stability effervescent, capsule, powder, and skincare formulations.
In-house formulation chemists create custom flavor profiles, color aesthetics, and active combinations with physical samples shipped in as fast as 7 days.
Full regulatory compliance assistance for import registration across Southeast Asia, Middle East, Europe, and FDA export compliance.
Sourcing effervescent tablets requires deeper technical diligence than standard capsule production due to the extreme moisture sensitivity of effervescent reactions. When evaluating potential factories, global procurement officers should audit against four key manufacturing pillars:
Inquire whether the factory operates dedicated environmental air handlers for effervescent production lines. Standard air conditioning is insufficient. The facility must present continuous environmental monitoring logs proving relative humidity is held below 20% RH during weighing, granulating, compression, and tube-filling operations.
Effervescent powders require specialized wet or dry granulation (such as fluid bed drying or roller compaction) to ensure uniform bulk density. Uniform particle sizing prevents component segregation during high-speed tableting, ensuring every single tablet contains the precise milligram dosage specified on your retail box.
Primary packaging is the final guardian of product shelf-life. Top suppliers utilize high-grade aluminum tubes equipped with desiccant-filled push caps containing silica gel or molecular sieves. The cap must form a hermetic seal upon automated insertion to continuously absorb residual micro-moisture trapped inside the head space.
For brands exporting to tropical regions (Hot & Humid Zone IVb), suppliers must supply 6-month accelerated stability data (40°C ± 2°C / 75% RH ± 5% RH). This guarantees that tablets will not expand, discolor, or lose effervescent potency inside retail warehouses.
Clear, authoritative answers to common inquiries from brand owners, buyers, and supply chain managers.
Partner with a verified GMP & ISO contract manufacturer. Request instant product specifications, sample kits, and OEM pricing directly from our technical team.
