Top China Probiotic Capsules Manufacturers & Factory

Strategic B2B Sourcing Guide: High-CFU Microencapsulation, Acid-Resistant Vegan Shells, cGMP Contract Manufacturing & Global Regulatory Compliance
Contract Manufacturing Portfolio

Featured OEM Probiotic & Nutraceutical Solutions

Explore our premium turnkey formulations and bulk manufacturing capabilities. Custom strain blends, targeted gastro-enteric delivery, and market-ready private label packaging.
Private Label Plant-Based Protein Powder
Clean-label vegan protein fortified with digestive enzyme complexes and heat-stable probiotic spores for optimal absorption and gut synergy.
OEM Creatine Monohydrate Powder
Ultra-pure 200-mesh micronized creatine monohydrate engineered for fast dissolution and enhanced athletic stamina, manufactured under cGMP standard.
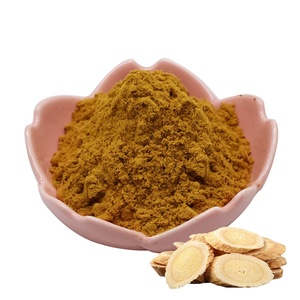
Astragaloside IV Powder
High-purity bio-active botanical extract for cellular longevity and immune system modulation, standardized for consistent batch potency.
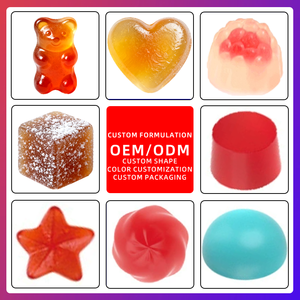
Gummy Supplements Manufacturing
Pectin-based, non-melting probiotic and multivitamin gummies with custom natural fruit flavors and precise active ingredient dosing.
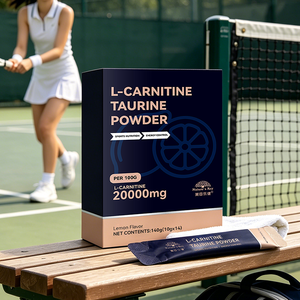
L-Carnitine Taurine Energy Powder
Metabolic acceleration complex combining L-Carnitine, taurine, and prebiotic fiber for clean energy, endurance, and gut microbiota balance.
Professional Salon Grade Shampoo
Microbiome-friendly scalp care and salon-strength hair repair formulas crafted with botanical oils and bio-fermented active ingredients.
Taurine Tablets Adult Healthcare Supplement
Vegan, gluten-free taurine tablets optimized for cardiovascular support and cellular hydration, packaged in eco-friendly private label bottles.
Mineral Premix for Multi-Species Animal Nutrition
Highly bioavailable multi-trace mineral premix formulated for pet nutrition and commercial livestock health, meeting international safety protocols.
Industry White Paper Report

The State of Probiotic Capsule Manufacturing in China

The global market for dietary supplements has undergone a fundamental shift toward precision microbiome interventions. As consumer awareness regarding gastrointestinal health, gut-brain axis modulation, metabolic wellness, and immune resilience expands, the demand for high-potency, shelf-stable probiotic capsules has accelerated exponentially. Among international contract manufacturing hubs, China has established itself as the undisputed epicenter for probiotic strain fermentation, microencapsulation innovation, and high-capacity capsule production.

Sourcing probiotic capsules requires an authoritative understanding of pharmaceutical-grade bio-processing. Unlike conventional vitamin or herbal solid-dose supplements, live probiotic microorganisms (such as Lactobacillus, Bifidobacterium, and spore-forming Bacillus species) are sensitive biological entities vulnerable to moisture, ambient temperature, atmospheric oxygen, and stomach acid degradation. Partnering with a premier Chinese probiotic capsule manufacturer ensures access to state-of-the-art industrial infrastructure—including 50,000-liter deep-tank anaerobic fermenters, ultra-low temperature freeze-drying systems, and humidity-controlled cleanroom encapsulation facilities operating under strict Class 100,000 (ISO Class 8) air quality standards.

Strategic Information Gain: Sourcing from top-tier Chinese probiotic factories provides B2B brand owners with an average 40% reduction in production lead times and access to high-density strain freeze-dried powders ($>5 \times 10^{11} \text{ CFU/g}$), guaranteeing end-of-shelf-life CFU counts rather than mere input claims at the time of manufacture.

50B+
CFU Shelf-Life Guarantee
20+
Years OEM/ODM Expertise
< 0.15
Water Activity ($a_w$) Control
100%
cGMP & ISO 22000 Compliant

Advanced Technical Innovations in Probiotic Capsule OEM

The commercial viability of a probiotic supplement brand relies on strain viability preservation. Leading Chinese factories have pioneered multiple technological barriers to shield delicate bacteria through production, transit, retail storage, and gastric passage.

Dual-Layer Microencapsulation

Utilizing lipid-protein matrix coating technology, live strains are wrapped in a protective micro-shell prior to encapsulation. This guards the cell wall against oxidative stress and environmental humidity, resulting in superior ambient stability without mandatory cold-chain logistics.

Enteric pH-Targeted Release Shells

Standard gelatin capsules dissolve in stomach acid within 15 minutes, killing up to 90% of non-spore strains. OEM factories utilize acid-resistant HPMC (Hydroxypropyl Methylcellulose) or Pullulan vegetarian capsules that remain intact in gastric juice (pH 1.2-2.0) for 2 hours, releasing live strains directly into the alkaline intestine (pH 6.8+).

Desiccant & Nitrogen Flush Packaging

Moisture is the primary enemy of freeze-dried bacteria. Advanced contract manufacturers implement automated nitrogen purging to reduce relative oxygen content below 1% and seal capsules in cold-form ALU-ALU blisters or specialized high-density desiccated polymer bottles with low water vapor transmission rates (WVTR).

Comparative Analysis: Capsule Delivery Systems

Understanding the operational and technical differences between capsule formats is critical for brand positioning and product efficacy:

Performance Specification Standard Bovine Gelatin Capsule Standard Plant HPMC Capsule Acid-Resistant Enteric HPMC Capsule Microencapsulated Acid-Resistant Capsule
Gastric Acid Resistance (pH 1.2) Poor (< 15 mins survival) Moderate (15–30 mins) Excellent (> 120 mins intact) Maximum (100% Target Targeted Bypass)
Moisture Content (Capsule Shell) 13.0% – 16.0% 4.5% – 6.5% 4.0% – 5.5% Ultra-Low (< 3.0%)
Room Temp Stability (24 Months) Requires Refrigeration Moderate Degradation High Viability Kept Shelf-Stable (No Cold-Chain Required)
Target Audience Appeal Traditional / Low Cost Vegetarian / Vegan Premium Health & Wellness Clinical & Clinical-Grade Formulations
Market Intelligence & Strategy

Probiotic Capsule Development Trends (2025–2030)

To gain a competitive edge, brand owners must align their product roadmaps with emerging science and changing consumer preferences. Probiotic capsule formulation is rapidly evolving from generic digestive aids toward target-specific bio-therapeutics.

1. Synbiotic & Tri-Phase Formulations

Modern brand innovation focuses on combining live probiotics with prebiotic fibers (such as Inulin, Fructooligosaccharides FOS, or Xylooligosaccharides XOS) and postbiotics (heat-treated beneficial bacterial metabolites like short-chain fatty acids). Advanced dual-chamber capsules or multi-pellet capsule-in-capsule technology enable the simultaneous delivery of incompatible actives without compromising strain stability.

2. Spore-Forming Strains & Extreme Stability

Spore-forming probiotics, such as Bacillus coagulans, Bacillus subtilis, and Bacillus clausii, possess a natural protective endospore structure. Sourcing spore-based capsules allows brands to create functional combinations with harsh botanicals, minerals, or vitamins while guaranteeing 100% room-temperature stability and survival through heat processing.

3. Condition-Specific & Psychobiotic Targeting

Broad-spectrum gut health claims are giving way to targeted health axes. Top Chinese OEM manufacturers now offer clinically researched strain blends specifically tailored for:

  • Gut-Skin Axis: Strains targeting acne, eczema, and skin hydration.
  • Psychobiotics: Strains for stress response, sleep quality, and cortisol modulation.
  • Women’s Vaginal Health: Lactobacillus rhamnosus & Lactobacillus reuteri combinations.
  • Metabolic & Weight Management: Strains engineered for GLP-1 pathway support and lipid regulation.

4. Clean-Label & Organic Certification Standards

Consumers increasingly demand total transparency. Leading factories have eliminated synthetic excipients (such as magnesium stearate, silicon dioxide, and titanium dioxide), replacing them with natural flow agents like organic rice concentrate, acacia gum, and natural chlorophyll or purple carrot-colored capsule shells.

Global Sourcing & Procurement Trends for B2B Buyers

Navigating international supply chains requires a balanced strategy between cost efficiency, speed-to-market, and rigorous quality control. China’s probiotic manufacturing ecosystem offers unmatched scale, but successful brand deployment hinges on strategic contract planning.

Why Top Global Brands Partner with Chinese Probiotic Factories

China's investment in industrial biotechnology has created a powerful manufacturing footprint. Key procurement advantages include:

  • Vertical Integration: Access to primary strain fermentation facilities, reducing intermediary raw material markups by up to 35%.
  • Agile Customization: Low minimum order quantities (MOQs starting as low as 30,000–50,000 capsules) for bespoke custom strain ratios compared to Western contract manufacturers requiring 500,000+ units.
  • Rapid Sampling & Prototyping: Express pilot batch creation within 7 working days, allowing brands to conduct consumer trials and stability validation quickly.
  • Comprehensive Export Documentation: Native handling of Certificate of Free Sale (CFS), Halal, Kosher, cGMP, and FDA facility registrations for seamless customs clearance worldwide.
Manufacturing Excellence

Why ProTech Health Sciences is Your Premier OEM Partner

With over two decades of dedicated health supplement, skincare, and nutraceutical manufacturing experience, ProTech Health Sciences offers a full-service, end-to-end contract manufacturing infrastructure engineered to scale global health brands.

Pharmaceutical-Grade R&D

Our in-house team of microbiological scientists and formulation engineers continuously develop stable multi-strain compounds tailored to target regional regulatory frameworks.

International Certifications

Fully equipped with cGMP, ISO 22000, ISO 9001:2015, HACCP, FDA Registration, and Halal Certifications, ensuring friction-free global distribution.

Rigorous Quality Protocol

Every batch undergoes 16S rRNA gene identification, flow cytometry live cell counting, heavy metal screening, pathogen testing, and real-time stability monitoring.

Procurement Guide

Frequently Asked Questions (FAQ)

Q1: How do China probiotic manufacturers guarantee CFU potency at the end of shelf life?
To guarantee live Colony Forming Unit (CFU) counts through a 24-month shelf life, manufacturers build in a scientific "overage" factor during formulation (typically 15% to 30% additional CFU input). Furthermore, factories maintain ultra-low relative humidity (< 30% RH) in cleanrooms, employ microencapsulation, use low-moisture plant HPMC capsules, and package products in nitrogen-purged ALU-ALU blister foil or bottles with integrated desiccant caps.
Q2: What is the Minimum Order Quantity (MOQ) for custom probiotic capsule manufacturing?
Standard OEM production MOQs typically start at 30,000 to 50,000 capsules per SKU for standard stock strain formulations. For completely custom strain blending, unique capsule colors, or bespoke enteric coatings, MOQs generally range from 100,000 to 300,000 capsules depending on raw material sourcing parameters.
Q3: Are plant-based vegetarian options available for probiotic capsules?
Yes, we offer multiple vegetarian and vegan hard-shell options, including standard HPMC capsules, acid-resistant HPMC capsules (DRcaps format), and premium Pullulan capsules derived from natural tapioca fermentation. All plant-based options are Non-GMO, allergen-free, Kosher, and Halal suitable.
Q4: How long does the turnkey OEM process take from concept to shipment?
The standard turnaround timeline is structured as follows:
  • R&D & Sample Approval: 7 – 10 working days.
  • Packaging Design & Printing: 10 – 14 working days.
  • Mass Capsule Production & Blistering: 15 – 20 working days.
  • Total Production Lead Time: Approx. 30 to 35 days from finalized artwork and deposit receipt.
Q5: What documentation is provided for international regulatory compliance?
We provide comprehensive technical dossier support, including Certificate of Analysis (COA) for every batch, Full Microbial & Heavy Metal Testing Reports, Certificate of Free Sale (CFS), cGMP Manufacturing Certificate, ISO 22000 & HACCP Documentation, BSE/TSE Free Statements, Allergen Declarations, and Stability Testing Protocol reports for product registration in target countries.
Q6: Do probiotic capsules require cold-chain refrigerated shipping?
With modern dual-layer microencapsulation technology and low-activity packaging, standard probiotic capsules can be safely transported via ambient ocean or air freight without cold chain requirements, provided ambient temperatures do not exceed 25°C–30°C for extended periods. For extreme climate destinations or high-sensitivity clinical strains, temperature-controlled insulated shipping solutions are available upon request.
Q7: Can custom probiotic strains or customer-supplied raw ingredients be used?
Yes. We offer both turnkey formulations and toll manufacturing services. If you have proprietary strain patents or specific branded raw materials, our factory can receive, audit, test, and encapsulate your raw materials according to your exact formulation instructions under strict Non-Disclosure Agreements (NDA).
Q8: How is water activity ($a_w$) managed during the capsule filling process?
Water activity is the single most critical parameter governing freeze-dried strain survival. Our manufacturing facility utilizes HVAC dehumidification systems to maintain strict environmental cleanroom conditions ($RH < 35\%$, Temp $20\pm2^\circ\text{C}$). Every finished batch is tested using digital water activity meters to ensure $a_w \le 0.15$, preventing premature strain reactivation and enzymatic destruction.

Ready to Launch Your High-Potency Probiotic Line?

Partner with China’s premier GMP-certified probiotic capsule factory. Get instant access to custom strain blending, free sample prototyping, and comprehensive B2B contract pricing.