Explore our premier range of custom dietary supplements, concentrated plant extracts, and personal care formulations engineered under strict international quality benchmarks.
Empowering global supplement brands with end-to-end OEM/ODM capabilities, certified cleanrooms, and stringent analytical rigor.
Operated under strict pharmaceutical-grade protocols including cGMP, ISO 22000, ISO 9001:2015, HACCP, FDA facility registration, and Halal certification to ensure total regulatory acceptance worldwide.
Our state-of-the-art laboratory features Supercritical CO2 extraction, High-Performance Liquid Chromatography (HPLC), and Mass Spectrometry to guarantee marker compound purity and zero solvent residues.
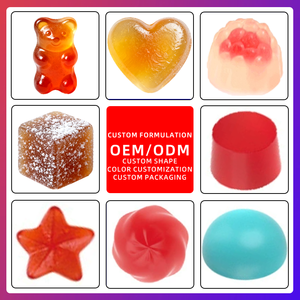
From botanical raw material processing to finished capsules, tablets, sachets, functional gummies, and cosmetics — we offer a turnkey solution including custom formula design and rapid prototyping.
We provide full technical documentation including Certificates of Analysis (COA), Heavy Metal ICP-MS reports, Pesticide Residue LC-MS/MS screenings, Stability Data, and Product Registration assistance.
Every plant extract batch is traceable back to its botanical source harvest. We enforce rigorous GAP (Good Agricultural Practices) to eliminate species cross-contamination and guarantee authentic botanicals.
Optimized manufacturing lines allow rapid sample delivery within 7 working days, alongside flexible MOQs tailored for scaling digital D2C healthcare brands and enterprise global distributors.
The global market for high-purity botanical extracts, active phytochemical ingredients, and functional dietary supplements is undergoing a fundamental structural transformation. Driven by heightened consumer demand for functional bio-actives, clean-label transparency, and stringent regulatory oversight from global authorities such as the US FDA, European Medicines Agency (EMA), and EFSA, business buyers must navigate a complex sourcing environment. China remains the world’s primary production hub for standardized plant extracts, producing over 80% of the global volume of active phytochemicals such as Ginsenosides, Astragaloside IV, Green Tea EGCG, Resveratrol, and Herbal Polysaccharides.
Traditional solvent-based thermal maceration is rapidly being phased out in favor of green, low-temperature, and high-efficiency extraction methodologies. Modern B2B procurement managers evaluating Chinese manufacturers must scrutinize the technical infrastructure deployed in factories:
Eliminates organic solvent residues entirely. Ideal for lipophilic phytocompounds, oil-soluble vitamins, and volatile essential oils. Delivers unmatched purity while preserving heat-sensitive bioactive compounds.
Utilizes specific cellulases and pectinases to break plant cell walls, dramatically increasing the yield of intracellular flavonoids and alkaloids while maintaining natural molecular integrity.
Reduces thermal degradation by utilizing cavitation energy. Accelerates mass transfer rates, enabling high concentration ratios (e.g., 50:1, 100:1) with reduced energy consumption.
Replaces high-temperature evaporation with ceramic microfiltration and reverse osmosis membranes, enabling cold concentration that locks in volatile aromatic and bioactive marker fractions.
As nutraceutical and cosmetics brands scale their private label product lines, sourcing strategies must evolve beyond simple price-per-kilogram metrics. Strategic advantage in 2025 and beyond will be dictated by three core pillars:
Raw botanical powders frequently suffer from low oral bioavailability due to poor water solubility or intestinal degradation. Premium OEM manufacturers are integrating specialized delivery systems directly during the raw material synthesis phase. Technologies such as Liposomal Encapsulation, Phytosome Complexes (binding extracts with phospholipids), and Spray-Dried Cyclodextrin Inclusion Compounds ensure active ingredients cross biological membranes effectively, giving consumer products a verifiable clinical edge.
Global border rejections are heavily triggered by trace contaminants. Leading manufacturers in China now implement 100% batch testing using Inductively Coupled Plasma Mass Spectrometry (ICP-MS) for heavy metals (Lead, Arsenic, Cadmium, Mercury) and LC-MS/MS triple-quadrupole systems for screening over 400 pesticide residues down to parts-per-billion (ppb) detection limits. Furthermore, monitoring Polycyclic Aromatic Hydrocarbons (PAHs) and Pyrrolizidine Alkaloids (PAs) has become mandatory for European Union compliance.
Brands are shifting away from buying single raw ingredients toward sourcing finished, multi-component functional premixes. Whether formulating sports nutrition blends containing Creatine Monohydrate and L-Carnitine, or cognitive anti-aging products utilizing Astragaloside IV and Taurine, relying on a unified ODM factory that handles ingredient blending, micro-granulation, tableting, or gummy production drastically reduces supply chain risk and time-to-market.
Essential insights for procurement directors, product developers, and regulatory specialists sourcing plant extracts from China.
We utilize a multi-tier authentication process. Initial identity verification is performed via Thin-Layer Chromatography (TLC) and DNA Barcoding to confirm species authenticity (e.g., distinguishing Astragalus membranaceus from inferior species). Active markers are quantified using High-Performance Liquid Chromatography (HPLC) calibrated against USP or EP reference standards. Additionally, H-NMR spectroscopy is conducted to rule out economic adulteration with synthetic active constituents or undeclared pharmaceutical ingredients.
Every production lot is issued a comprehensive COA detailing: (1) Physical Assay: Color, odor, particle size (mesh distribution), bulk density, loss on drying, and ash content; (2) Chemical Assay: Active marker compound assay percentage by HPLC/UV; (3) Contaminant Testing: Heavy metals (Pb, As, Cd, Hg via ICP-MS), pesticide residue screen (USP/EP compliant), residual solvents (via Headspace GC-MS), and microbiological profile (Total Plate Count, Yeast & Mold, Salmonella, E. coli, Staphylococcus aureus).
Yes. We provide specialized physical processing services including micronization (down to 200–500 mesh for beverages and sports powders), fluid-bed instantization (granulation for cold-water instant solubility), spray-drying, and custom oil-to-powder microencapsulation. This allows lipophilic ingredients to dissolve cleanly into functional beverages without sedimentation.
For standard standardized extract powders available in warehouse stock, MOQs start as low as 1 kg to 25 kg (standard fiber drum). For custom contract OEM formulations (tablets, capsules, functional gummies, or complex premixes), standard MOQs range from 50,000 capsules/tablets or 500 kg of bulk powder. Pilot sample batches for laboratory evaluations are typically dispatched within 5 to 7 working days.
Our regulatory team prepares complete customs clearance documentation customized for target markets, including Health Certificates, Certificate of Origin (Form E/CO), BSE/TSE-Free Declarations, Non-GMO Statements, Safety Data Sheets (SDS), and FDA Food Facility Registration numbers. We maintain long-term freight partnerships to offer DDP (Delivered Duty Paid), CIF, or FOB terms worldwide.
Contact our R&D specialists and procurement team today to request custom quotes, technical specification sheets, or pilot laboratory samples for your next formulation.
