Industrial-grade nutraceuticals, cosmeceuticals, and veterinary feed additives manufactured under strict cGMP and ISO 22000 quality management standards.
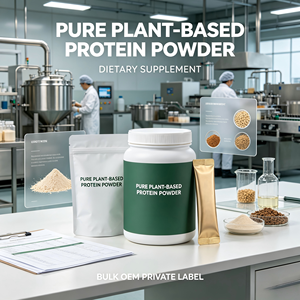
Hypoallergenic organic pea, brown rice, and pumpkin seed protein blend engineered for optimal amino acid profiling and rapid cold-water dispersion.
Ultra-pure 200-mesh micronized creatine monohydrate designed for rapid cellular ATP regeneration, maximum muscle hydration, and zero solubility residue.
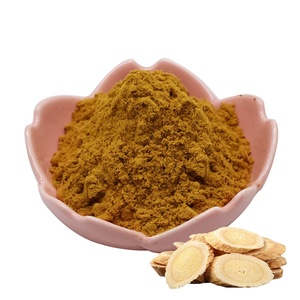
Pharmaceutical-grade standard bioactive extract from Astragalus Membranaceus, targeted for cellular longevity, telomere maintenance, and immune support.
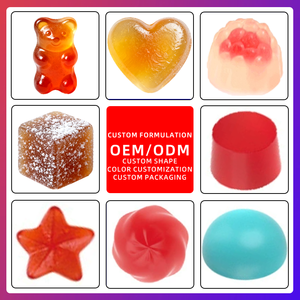
Pectin-based, heat-stable functional vitamin gummies with zero sugar coating options. High loading capacity for multivitamins, minerals, and botanicals.
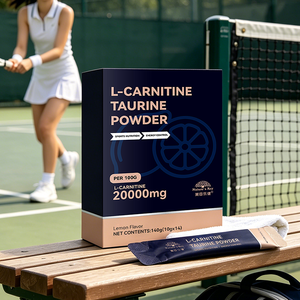
Synergistic fatty-acid transport matrix combining L-Carnitine L-Tartrate, pure Taurine, and Polydextrose prebiotic fiber for thermogenic energy support.
Sulfate-free keratin and amino-acid enriched hair care formulation engineered for structural cortex repair, color protection, and scalp barrier restoration.
High-density compressed tablet matrix with controlled disintegration parameters. Supports cardiovascular health, neuro-protection, and cellular osmoregulation.
Highly bioavailable chelated trace mineral premix (Zinc, Copper, Manganese, Selenium) tailored for livestock and pet food fortification.
ProTech Health Sciences operates state-of-the-art cGMP certified cleanrooms and automated high-throughput production lines to bridge formulation science with global scalability.
Our Class 100,000 cleanroom environments adhere strictly to US FDA 21 CFR Part 111 and EU EudraLex Volume 4 standards, preventing cross-contamination via HEPA positive-pressure air filtration and environmental humidity controls.
Equipped with High-Performance Liquid Chromatography (HPLC), Gas Chromatography-Mass Spectrometry (GC-MS), and Atomic Absorption Spectroscopy (AAS) to verify active ingredient potency, heavy metals, pesticides, and residual solvents.
Our regulatory affairs team streamlines market entry across North America, Europe, Southeast Asia, and the Middle East by generating technical dossiers, HALAL JAKIM/MUI documentation, Certificate of Free Sale (CFS), and FDA MoCRA listings.
The global contract manufacturing ecosystem is undergoing a fundamental transformation driven by biotechnology breakthroughs, stringent regulatory shifts, and consumer demand for absolute ingredient transparency.
Institutional buyers are demanding end-to-end supply chain visibility. Modern OEM factories must provide batch-specific blockchain tracking from botanical farm origin or bio-fermentation tank to final encapsulation, eliminating adulteration risks.
Procurement preference is shifting away from traditional synthetic binders like magnesium stearate, silicon dioxide, and artificial colorants toward natural plant cellulose, rice hull concentrates, and organic fruit-derived flavor carriers.
Next-generation OEM suppliers are integrating liposomal delivery systems, phytosome complexes, and microencapsulation technologies to enhance the intestinal absorption rate of lipid-insoluble actives by up to 800%.
Selecting the appropriate contract manufacturing model is critical for brand equity, intellectual property protection, and speed-to-market execution.
| Evaluation Parameter | OEM (Original Equipment Manufacturing) | ODM (Original Design Manufacturing) | ProTech Hybrid Solution |
|---|---|---|---|
| Formulation Ownership | 100% Brand Proprietary IP | Manufacturer Shared IP Library | Flexible IP Transfer Protocols |
| R&D Lead Time | 4 - 8 Weeks (Formulation Development) | 1 - 2 Weeks (Off-the-Shelf) | Express Sampling (7 Days) |
| Minimum Order Quantity (MOQ) | Higher (50,000 Capsules / 500kg Powder) | Lower (3,000 Units Standard) | Scalable Tiered Pilot Batches |
| Customization Degree | Unlimited (Actives, Excipients, Delivery) | Limited (Packaging & Flavor Only) | Full Tailored Matrix Engineering |
| Regulatory Risk Mitigation | Brand Responsible for Stability Data | Manufacturer Pre-Validated Formulas | Turnkey Dossier & Stability Guarantee |
Our 5-stage quality assurance protocol ensures that every production batch meets rigorous pharmaceutical and food-safety specifications prior to global release.
Quarantine verification via Fourier-Transform Infrared Spectroscopy (FTIR) identity testing, heavy metal ICP-MS screening, and allergen quantification.
Continuous monitoring of tablet hardness, friability, disintegration speed, powder bulk density, and capsule weight variation within ±1.5% margins.
HPLC quantitative testing confirming active compound potency matches 100% of label claims through the entire shelf-life duration.
Microbiological screening for E. coli, Salmonella, and Staphylococcus aureus alongside ICH Q1A(R2) accelerated stability testing under 40°C/75% RH.
Market analytical data indicates strong growth across specialized consumer health verticals. Our laboratory is equipped to formulate cutting-edge products across key functional segments.
Combining hydrolysed marine collagen peptides with bio-identical ceramic phytoceramides, hyaluronic acid, and astaxanthin to stimulate dermal fibroblast matrix regeneration and boost hydration from within.
Formulating synergetic adaptogenic matrices utilizing Alpha-GPC, Lion's Mane mushroom extracts, Bacopa Monnieri, and L-Theanine to optimize focus, neurotransmitter synthesis, and stress resistance.
Engineered multi-strain probiotic matrices utilizing heat-resistant Bacillus coagulans and Bacillus subtilis spores capable of surviving stomach acid environments without requiring refrigerated supply chains.
Enterprise procurement managers should evaluate prospective contract manufacturing facilities against these essential structural criteria prior to contract signing.
Confirm the facility uses HEPA filtration with a minimum of 20 air changes per hour and differential pressure monitoring between processing rooms.
Ensure key assays (HPLC, GC-MS) are performed in-house rather than outsourced to secondary labs, avoiding release delays.
Audit the supplier's Standard Operating Procedures (SOPs) regarding ingredient supplier substitutions and packaging material changes.
Verify physical separation protocols for common allergens (soy, dairy, shellfish, peanut) across storage, blending, and filling lines.
Check on-site environmental chambers for real-time (25°C/60% RH) and accelerated (40°C/75% RH) shelf-life validation capabilities.
Conduct a mock recall exercise during facility inspection to verify complete forward and backward batch tracing within 4 hours.
Technical, regulatory, and logistical answers to support commercial brand managers and supply chain directors.
Standard turnaround time for repeat orders is typically 20 to 30 business days from art approval and deposit receipt. For new custom formulations requiring bespoke lab pilot batches, analytical method validation, and stability testing, initial development lead times range from 4 to 6 weeks. Express R&D sampling routines can be accelerated to 7 business days using pre-validated stock active raw materials.
We execute legally binding bilateral Non-Disclosure Agreements (NDAs) prior to any formulation discussion. Under custom OEM agreements, all customized active ratios, proprietary premixes, and unique ingredient combinations remain the 100% exclusive intellectual property of the brand owner. Our manufacturing database is segregated to ensure proprietary client formulas cannot be commercialized for third parties.
MOQs vary depending on technical production constraints: Hard Gelatin/HPMC Capsules require a minimum of 30,000 to 50,000 units per run; Compressed Tablets require 50,000 units; Powder Blends start at 300kg total batch weight; Pectin Functional Gummies require 100,000 gummies; and Cosmeceutical Skincare Liquids/Serums start at 1,000 to 3,000 finished retail units per SKU.
Our manufacturing infrastructure holds cGMP (US FDA 21 CFR Part 111), ISO 22000:2018, ISO 9001:2015, HACCP, and HALAL (JAKIM/MUI compliant) certifications. We issue full technical regulatory documentation sets including Certificate of Analysis (COA), Certificate of Free Sale (CFS), Stability Protocol Reports, Ingredient Origin Statements, and Heavy Metal/Microbial Safety Clearances necessary for registration across EU, US, Middle Eastern, and ASEAN health authorities.
Yes, we provide full turn-key primary and secondary packaging solutions. This includes HDPE/PET bottles, glass tincture droppers, blister strips (Alu-Alu or PVC/PVDC), single-serve stick packs, sachet foil laminates, and sustainable PCR (Post-Consumer Recycled) eco-containers. Our design team ensures label artwork adheres to local regulatory label compliance laws, including font sizing, allergen disclosures, and nutrient reference value (NRV) tables.
Every commercial production lot is released only after undergoing thorough Quality Control audit. Each shipment includes a comprehensive batch Certificate of Analysis (COA) detailing physical parameters (weight variation, color, disintegration), active ingredient assay percentages (HPLC/UV-Vis tested), microbiological safety screening (Total Plate Count, Yeast & Mold, Pathogens), and heavy metal limits (Lead, Arsenic, Cadmium, Mercury).
