Explore our core cGMP-compliant formulations engineered for global market entry. Each product offers scalable MOQs, custom flavoring, bespoke packaging, and complete technical regulatory dossiers.
The landscape of global health product procurement has undergone a seismic shift. Modern brand owners, pharmaceutical distributors, and e-commerce leaders no longer evaluate contract manufacturers solely on unit price. Today, the competitive edge relies on Information Gain, rapid R&D iteration, strict international quality compliance, and robust supply chain infrastructure. As one of China's premier white-label factories, ProTech Health Sciences bridges the gap between raw botanical engineering and commercial market execution.
Strategic Takeaway: A successful OEM partnership requires evaluating a supplier's analytical laboratory assets, cGMP cleanroom classifications, raw material origin verification, and dynamic regulatory dossier preparation capacity.
Navigating China's vast industrial base requires distinguishing between simple commodity compounding plants and advanced contract research and manufacturing organizations (CRMOs). High-performing white-label suppliers operate certified Class 100,000 cleanrooms, maintain full batch-level traceability via ERP integration, and utilize high-performance liquid chromatography (HPLC) and gas chromatography-mass spectrometry (GC-MS) to guarantee active compound potency and safety across every batch.
Understanding the operational distinction between Original Equipment Manufacturing (OEM) and Original Design Manufacturing (ODM) is essential for maximizing gross margins and reducing time-to-market:
Ideal for established brands with existing proprietary formulations. You provide the exact Master Batch Record (MBR) and active specifications; we execute precision blending, encapsulation, tableting, or liquid filling under strict cGMP protocols.
Designed for brands entering new categories quickly. Leverage our library of 500+ pre-formulated, stability-tested, and market-validated health supplements, skincare products, and pet nutrition items to launch within weeks.
A complete end-to-end solution combining custom formulation development, primary/secondary structural packaging design, regulatory dossier registration support, and global freight management.
With over two decades of dedicated manufacturing mastery, ProTech Health Sciences stands as an industry benchmark among Chinese white-label suppliers. Our modern manufacturing complex incorporates multi-category automation lines capable of producing hard capsules, softgels, direct-compression tablets, multi-shape functional gummies, micro-encapsulated powders, and salon-grade topical cosmetics.
Entering strict regulatory territories such as North America, the European Union, Southeast Asia, and the GCC region requires compliance far beyond basic manufacturing. ProTech operates under a unified global quality matrix:
Formulation R&D Engine: Our in-house team of 30+ food scientists, biochemists, and cosmetic chemists provide rapid sampling turnaround—delivering customized physical samples to your doorstep in as few as 7 business days.
As consumer preferences evolve, brand owners sourcing from China must align their product development strategies with macro industry trends. Procurement leaders who capitalize on these technological shifts will secure higher market share and stronger brand equity.
Standard crude powders are rapidly being replaced by micro-encapsulated and liposomal delivery systems. Actives like Astragaloside IV, Creatine, and Curcumin exhibit up to 5x higher cellular uptake when processed through liposomal emulsion technology.
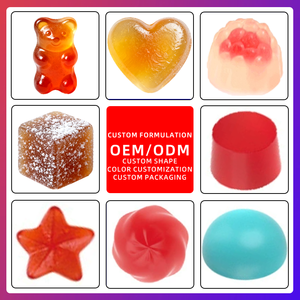
The global shift toward plant-based nutrition has elevated pectin and sodium alginate gummy matrices over traditional animal gelatin. Future-ready factories offer heat-stable, non-melting, low-sugar gummies with active vitamin & mineral loading.
Pet humanization is driving rapid expansion in private-label pet nutrition. High-growth segments include chelated trace mineral premixes, joint-support soft chews, and specialized botanical skin-and-coat conditioning formulas.
Global regulations are curbing single-use plastics. Sourcing trends prioritize Post-Consumer Recycled (PCR) HDPE bottles, aluminum refill canisters, and biodegradable stick-pack sachet films for powder formulas.
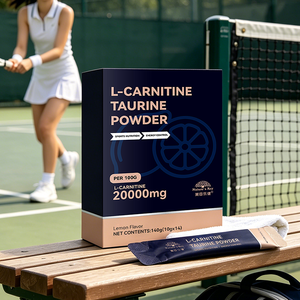
Single-ingredient supplements are evolving into complex synergistic formulas. Blends combining ergogenic compounds like L-Carnitine, Taurine, and direct osmoprotectants with prebiotic fibers dominate the active health space.
Leading Chinese white-label suppliers are introducing flexible initial production tiers. Lower MOQs allow brands to test market demand while retaining options for rapid scale-up upon proven retail traction.
Below are authoritative technical answers to common queries encountered when evaluating white-label factories and contract suppliers in China.
MOQs depend primarily on the dosage form and packaging format. Standard capsule and tablet formulations typically start at 3,000–5,000 retail bottles (or 100,000 bulk units). Custom powder stick-pack sachets start at around 10,000–20,000 sachets, while specialized gummy runs start from 3,000 bottles due to pectin batch sizing. For pilot runs and market testing, flexible tiered MOQs are available upon request.
We enforce strict, legally binding Non-Disclosure Agreements (NDAs) governed by international contract standards prior to receiving any formula details. Custom formulations engineered for your brand remain exclusively yours. Furthermore, our internal ERP system anonymizes active ingredient ratios on the production floor to prevent formulation leakages.
Our manufacturing infrastructure operates in compliance with cGMP (Good Manufacturing Practice), ISO 22000 (Food Safety Management System), ISO 9001:2015 (Quality Management), HACCP, and Halal certification standards. We are also FDA registered, allowing direct export of finished dietary supplements and personal care products into North American and European markets.
R&D custom sampling requires 7 to 10 working days. Once physical samples and packaging artwork are approved, commercial mass production generally takes 25 to 35 business days, including raw material quality verification, compounding, primary filling, secondary labeling, and final QC release testing.
Yes. Our regulatory affairs department assists global clients with comprehensive document dossiers including Certificates of Free Sale (CFS), Certificates of Analysis (COA), Stability Study Reports, Heavy Metal & Microbiological Lab Data, Ingredient Safety Data Sheets (MSDS), and Master Batch Records needed for local health authority filings (e.g., US FDA, EU CPNP, ASEAN cosmetic notifications, GCC Halal authorities).
Every active pharmaceutical ingredient (API), botanical extract, and functional excipient undergoes stringent quarantine upon arrival. Our QC laboratory performs identity testing (FTIR), purity assays (HPLC), heavy metal analysis (ICP-MS), pesticide residue screening, and pathogen testing before clearing materials for production lines.
