Explore our GMP and CE-certified contract manufacturing capabilities spanning chewables, custom powders, botanical extracts, and specialized dietary supplements engineered for global compliance.
The global nutraceutical landscape is experiencing a structural paradigm shift from conventional oral solid dosage forms (tablets and hard-shell capsules) toward functional, chewable delivery systems. Among these, CE certified multivitamin gummies represent the fastest-growing segment across European, North American, and Asia-Pacific markets. Modern consumers demand dietary supplements that eliminate pill fatigue while delivering precise micronutrient kinetics, superior organoleptic profiles, and clean-label integrity.
As an authoritative OEM/ODM factory, our technical R&D focuses heavily on rheological optimization and gelling matrix stability. The choice between citrus-derived Pectin and porcine/bovine Gelatin dictates not only thermal stability during transatlantic ocean freight but also dictates regulatory clearance within European markets under CE and EFSA frameworks.
A primary challenge in manufacturing high-potency multivitamin gummies lies in preventing micronutrient degradation during high-temperature thermal cooking processes (typically 105°C–115°C slurry boiling). Water-soluble vitamins (Ascorbic Acid, Thiamine, B12) and fat-soluble vitamins (Vitamin A Palmitate, Cholecalciferol D3, d-Alpha Tocopherol) display varying degradation kinetics when exposed to heat, shear force, and moisture.
To ensure 100% label claim verification throughout a 24-month shelf life, our factory implements proprietary Micro-encapsulation & Precision Overage Strategies:
| Technical Parameter | Citrus Pectin Matrix | Bovine/Porcine Gelatin | Sugar-Free Maltitol/Pectin |
|---|---|---|---|
| Melting Temperature (°C) | > 48°C (Heat Resistant) | 34°C - 37°C (Risk in transit) | > 45°C (Stable) |
| Optimum pH Processing Range | 3.2 - 3.5 (Acidic systems) | 4.0 - 7.0 (Neutral/Broad) | 3.1 - 3.4 (Strict control required) |
| Dietary / Regulatory Status | 100% Vegan, Halal, Kosher | Non-Vegan, Religious Restrictions | Keto-Friendly, Diabetic-Safe, Vegan |
| Hygiene & Moisture Absorption | Low Equilibrium Moisture | High Hygroscopicity (Clumping risk) | Ultra-Low Moisture Retention |
| EU / CE Market Clearance Rate | 99.4% Immediate Pass | 78.2% (Subject to TSE/BSE checks) | 98.8% (EFSA Compliant) |
As international buyers, brand owners, and pharmaceuticals evaluate contract manufacturing partners for 2025–2030, procurement strategy is evolving from simple per-unit cost negotiation to comprehensive supply chain risk mitigation, raw material traceability, and multi-jurisdictional compliance.
Importers are phasing out traditional high-fructose corn syrup (HFCS) and sucrose bases. The market is shifting decisively toward non-cariogenic sugar alcohols including Maltitol, Erythritol, and Soluble Tapioca Fiber (Isomalto-oligosaccharides), enabling tooth-friendly and diabetic-safe product claims.
Modern formulations no longer stop at basic RDA vitamins. B2B buyers are requesting complex hybrid formulas combining essential micronutrients with adaptogens (Ashwagandha), botanical extracts (Astragaloside IV), postbiotics, and nootropics (L-Theanine) within a single gummy architecture.
With tightening EU customs scrutiny, procurement teams require factories capable of providing full batch Certificate of Analysis (COA), heavy metal ICP-MS screening, pesticide testing, and verified compliance with EU Regulation (EC) No 178/2002 and CE regulatory criteria.
We combine advanced pharmaceutical manufacturing standards with commercial agility, providing brand owners with turnkey private label and custom ODM solutions from concept to customs clearance.
Our facility houses high-speed, fully automated German-engineered gummy mogul depositor systems capable of outputting over 10,000 kg of finished pectin and gelatin gummies per shift. Automated optical sorting ensures absolute weight uniformity (±0.05g variance) and zero visual defects.
All conditioning, oil-coating, drying, and bottle-filling operations take place within positive-pressure, HEPA-filtered cleanroom suites. Temperature is locked at 20°C ± 2°C with relative humidity controlled under 38% to prevent microbial contamination and product sticky phase transitions.
Equipped with High-Performance Liquid Chromatography (HPLC), Gas Chromatography-Mass Spectrometry (GC-MS), and Atomic Absorption Spectroscopy (AAS), our internal QA team tests raw materials, in-process slurries, and finished products for potency, heavy metals (Pb, Cd, Hg, As), and microbial limits.
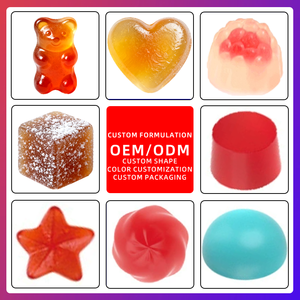
From classic bears, hearts, and stars to proprietary branded shapes, our 3D mold prototyping team turns ideas into physical production molds within 7 days. We provide comprehensive bottling, blister packaging, sachet filling, and custom label compliance clearance worldwide.
Detailed technical and operational answers tailored for procurement managers, brand founders, and wholesale buyers looking to manufacture CE certified gummies.
Partner with a premier contract manufacturer. Our technical R&D team and regulatory experts are standing by to assist with formulation development, sample requests, and wholesale quotes.
