Explore our state-of-the-art formulations available for custom contract manufacturing, private labeling, and bulk export. Formulated in GMP-certified, ISO Class 7 cleanrooms.
Understanding the technical requirements, quality benchmarks, and international compliance directives governing global functional food exports.
In the evolving global health market, obtaining CE Certification for functional food manufacturing is not merely a label—it represents a comprehensive validation of safety, health, and environmental protection standards aligned with European Conformity directives. As a premier CE-certified functional food factory, our infrastructure integrates EU Directive compliance directly into batch processing, continuous quality control, and automated packaging protocols.
Functional foods bridge the gap between traditional nutrition and pharmaceutical intervention. Consequently, manufacturing facilities must maintain stringent controls over active compound standardization, heavy metal residual limits, pesticide screening, and microbiological stability. Our facility utilizes High-Performance Liquid Chromatography (HPLC) and Gas Chromatography-Mass Spectrometry (GC-MS) to audit every production run from raw botanical intake to finished unit export.
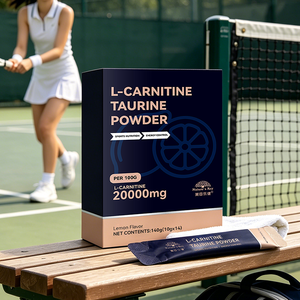
Bioavailability remains the single most critical differentiator in functional food efficacy. Raw nutrients such as hydrophobic phytonutrients, sensitive amino acids (e.g., L-Carnitine, Taurine), and volatile botanical extracts often suffer from premature degradation or low intestinal absorption.
Our R&D division employs advanced microencapsulation and spray-drying technologies to wrap sensitive bio-actives within protective lipid or polysaccharide matrices. This process guarantees:
| Quality Metric / Parameter | Standard OEM Manufacturer | ProTech CE Certified Enterprise Facility |
|---|---|---|
| Cleanroom Environmental Control | Standard ISO Class 8 or non-rated ambient | ISO Class 7 (100,000-Grade) HEPA Filtered Facilities |
| Analytical Testing Capabilities | Basic wet chemistry, third-party reliant | In-House HPLC, GC-MS, Atomic Absorption & Micro Lab |
| Regulatory Dossier Support | Basic Certificate of Analysis (COA) | Full EU Dossier, Halal, FDA Registration & Health Certificates |
| Formulation Turnaround & Sampling | 3–6 Weeks turnaround time | 7-Day Rapid Express Sampling & Formulation Prototyping |
| Traceability & Batch Auditing | Manual paper log tracking | Fully Automated MES & Barcode Supply Chain Traceability |
Over two decades of OEM/ODM manufacturing excellence, empowering international brand owners, distributors, and pharmaceutical importers.
Operate with complete market safety. Our production lines comply with CE marks, GMP, ISO 22000, ISO 9001:2015, HACCP, FDA registration, and Halal certification protocols for seamless global clearance.
Accelerate your product launch timeline. Tap into our extensive library of scientifically validated, stable formulations spanning plant proteins, sports nutrition, bio-active botanicals, and functional gummies.
From custom active ingredient sourcing to structural packaging design, product registration dossiers, and international sea/air freight management, we handle your entire supply chain.
Key insights for brand managers and purchasing directors looking to maintain competitive advantage in the next 5 years.
Consumer demand is moving away from synthetic isolate powders toward natural, enzymatic-hydrolyzed plant peptides with enhanced solubility and neutral flavor profiles.
Importers are demanding verified concentrations of specific bio-actives—such as Astragaloside IV at 10% or pure Creatine Monohydrate—rather than generic plant extracts.
Functional gummies are expanding beyond simple multivitamins to complex formulations containing thermogenic compounds, amino acids, and digestive enzymes while remaining sugar-free.
Global regulatory bodies are enforcing full farm-to-shelf traceability. Importers must align with CE-compliant factories capable of providing full analytical validation for every lot.
To optimize unit margins and prevent regulatory delay, global buyers should pivot toward OEM manufacturers offering dual-capability: in-house raw material standardization combined with integrated packaging lines. Contracting with a factory capable of executing both functional powder premixes and gummy delivery vehicles under one roof reduces supply-chain friction by up to 35%.
Direct answers to critical operational, legal, and manufacturing inquiries from corporate purchasers and brand owners.
Whether you require custom formulation development, bulk supply of standardized botanicals, or turnkey private label manufacturing, our senior R&D and export teams are ready to assist.
